
Industrial equipment for bulk materials
We supply industrial equipment for bulk materials, designed for conveying, dosing and controlled feeding in a wide range of production processes. Each product is developed for the specific requirements of the site, the material and the operating mode, which gives reliable and predictable operation.
Below are our main product groups. In each of them you will find different versions and technical solutions, and information on what we can build to your requirements.
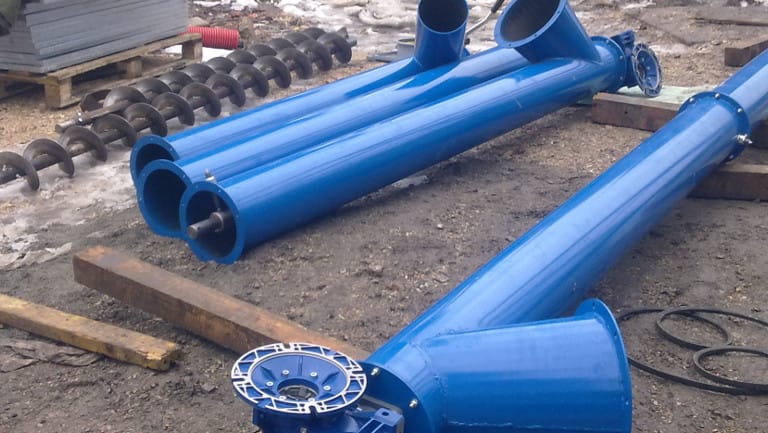
Screw conveyors
For conveying and dosing bulk and powdered materials.
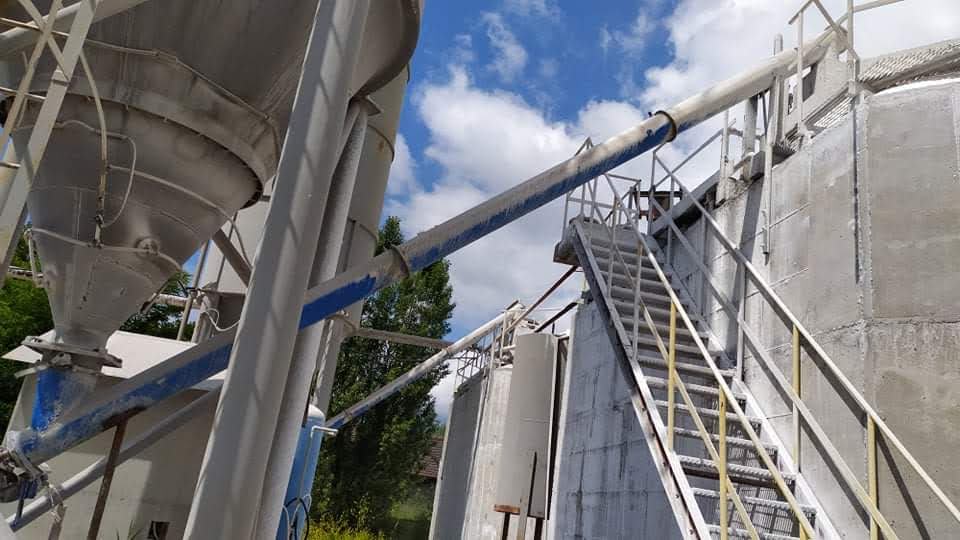
Tubular screw conveyors
Enclosed screw conveyors Ø60–630 mm for cement, flour, grain and pellets.
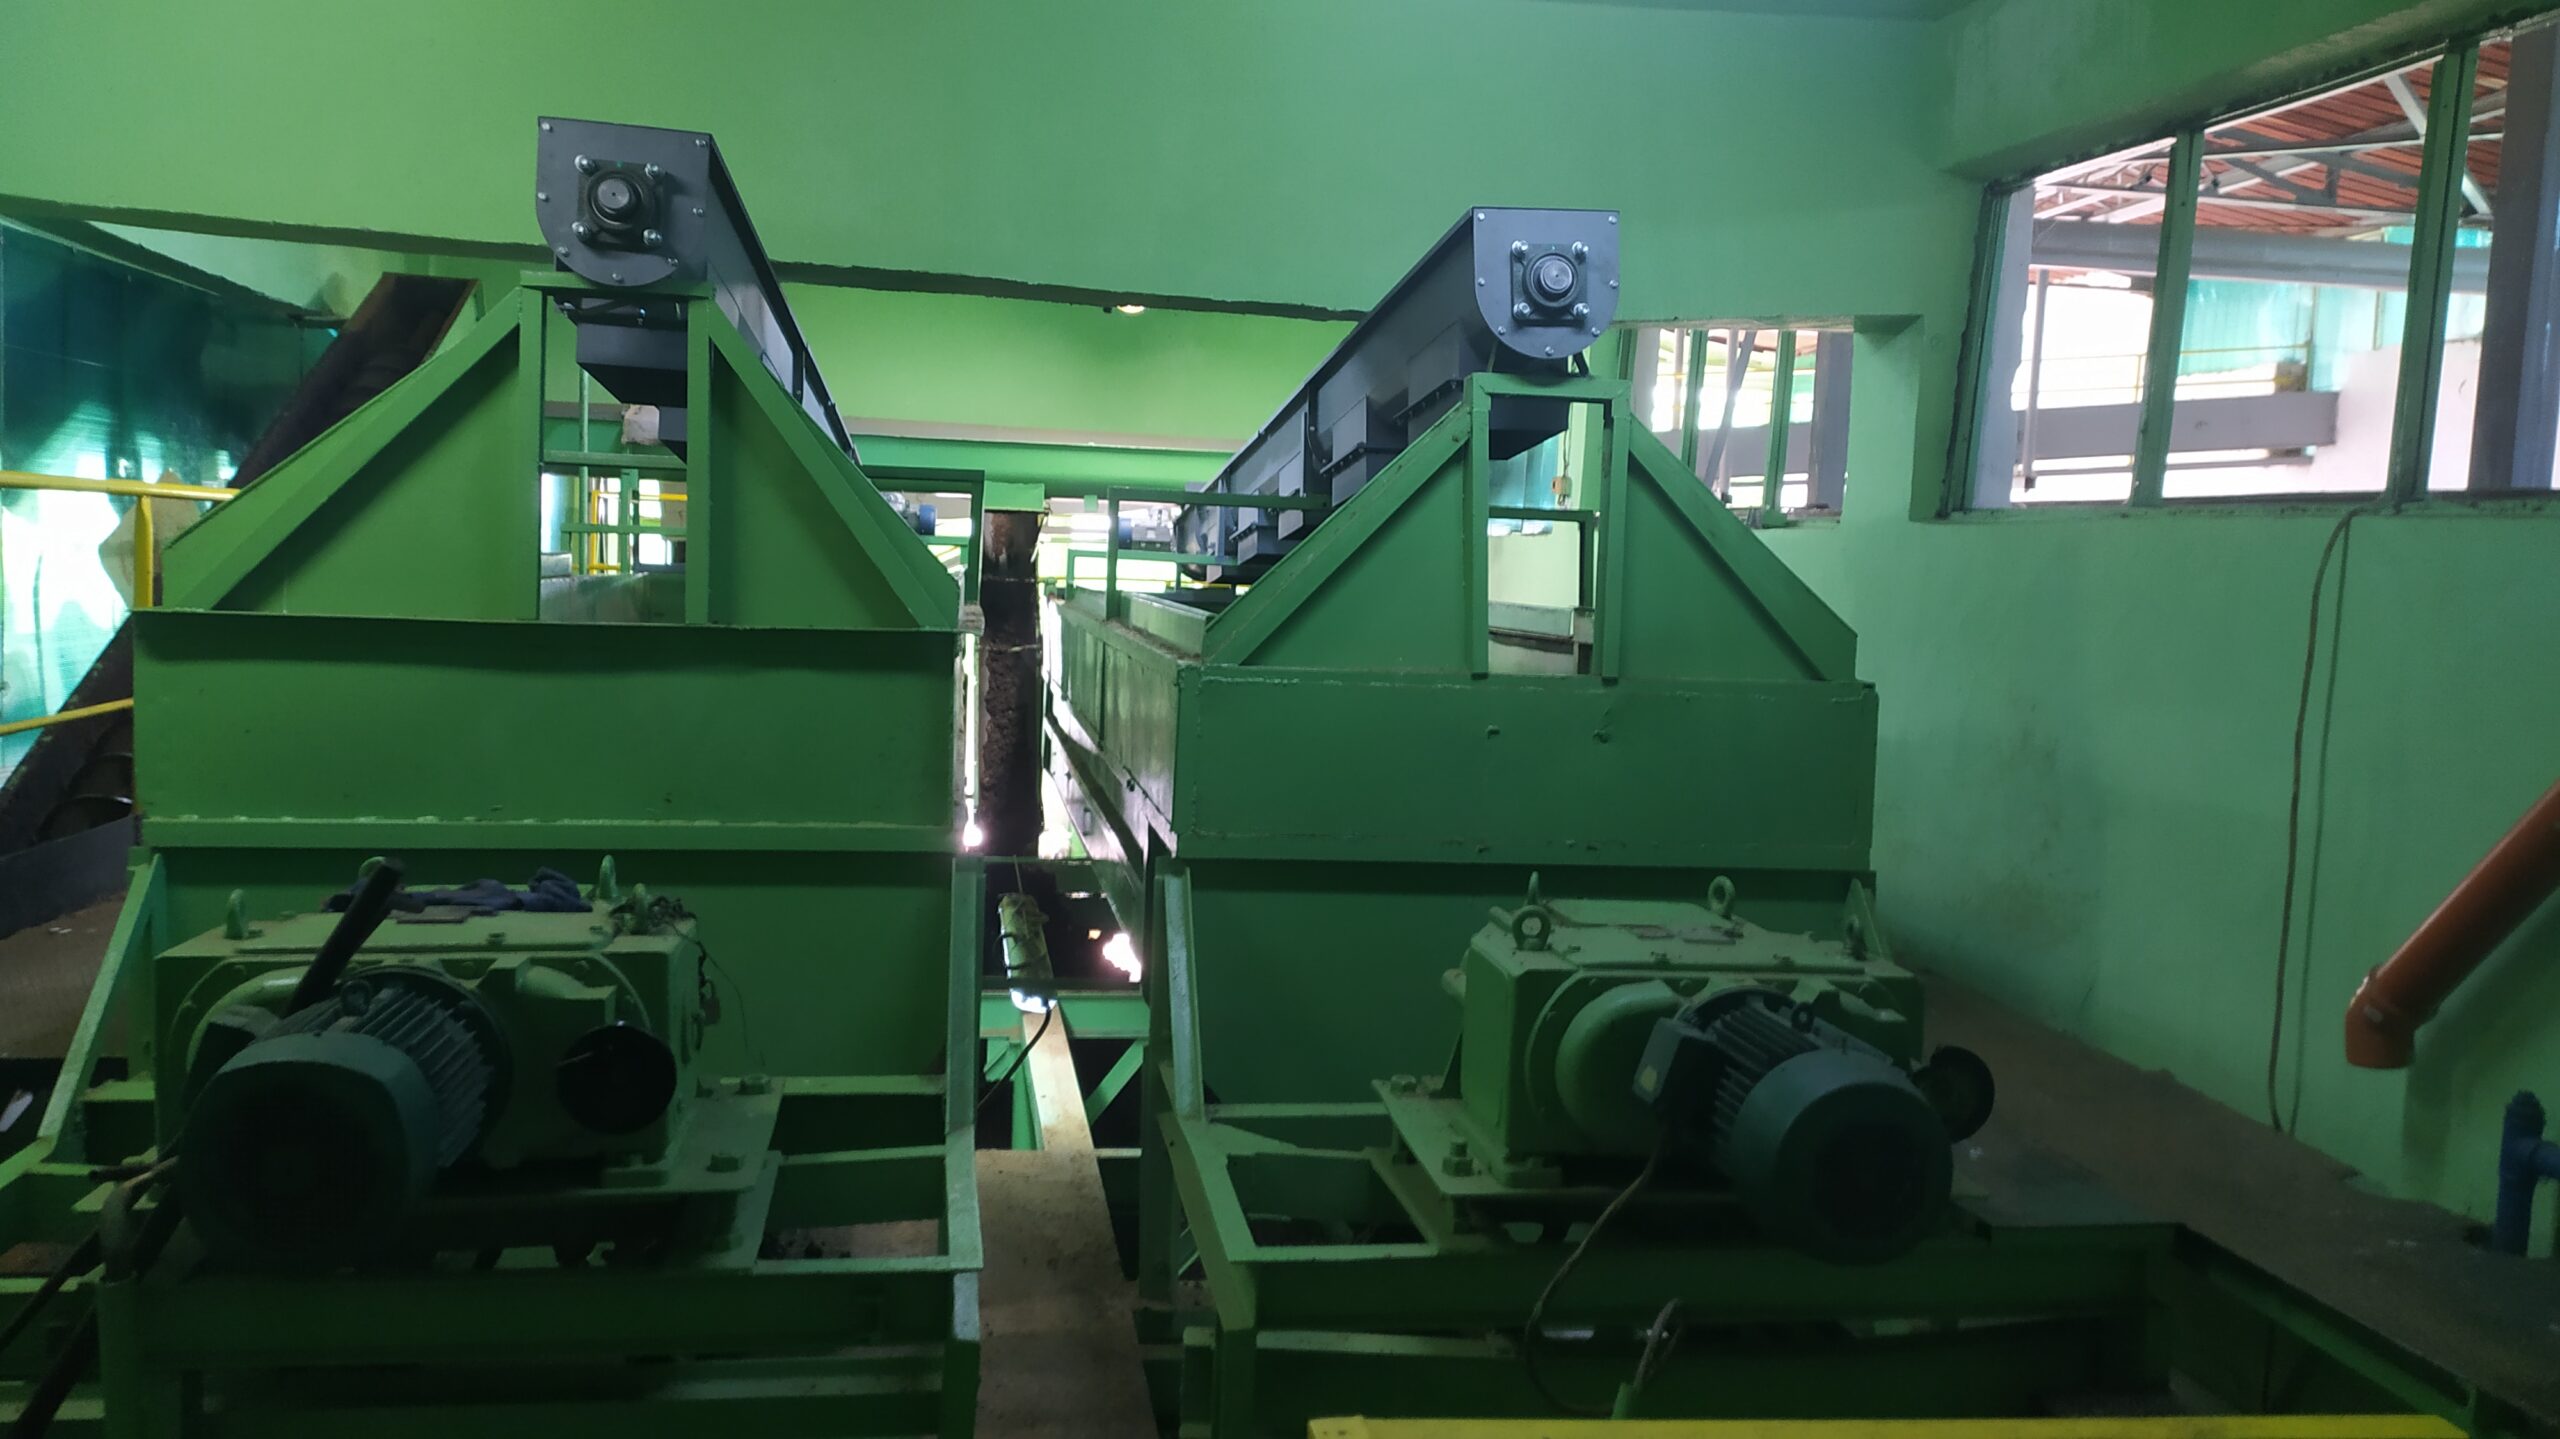
U-trough screw conveyors
U-trough screw conveyors for wet, sticky and coarse materials.
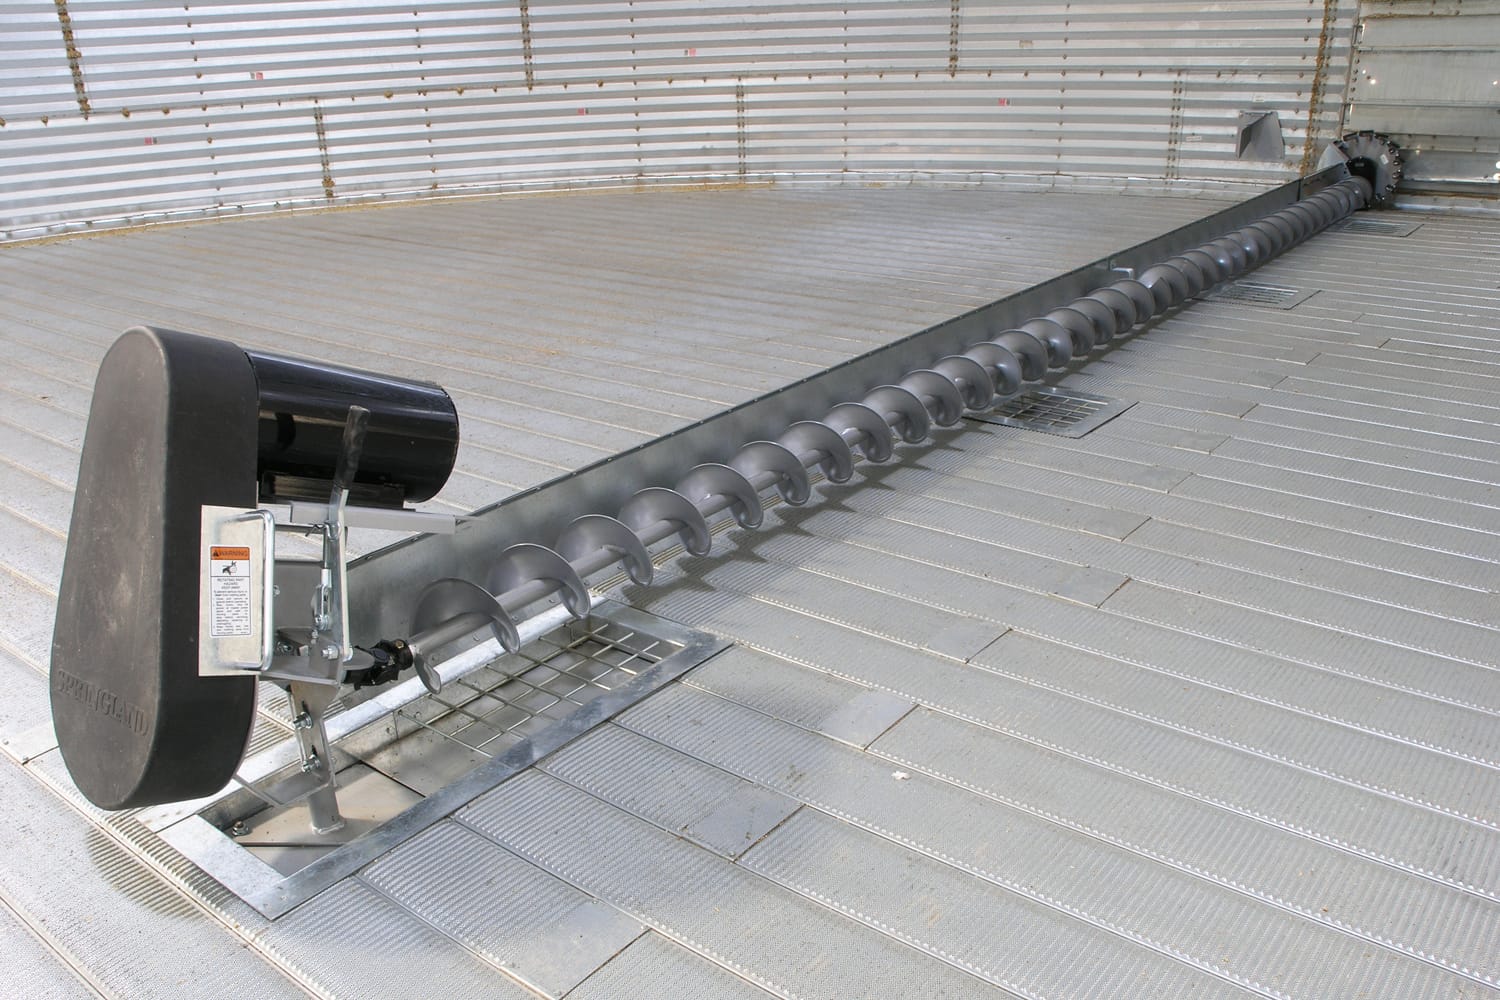
Sweep augers
For emptying flat-bottom silos – made to size.
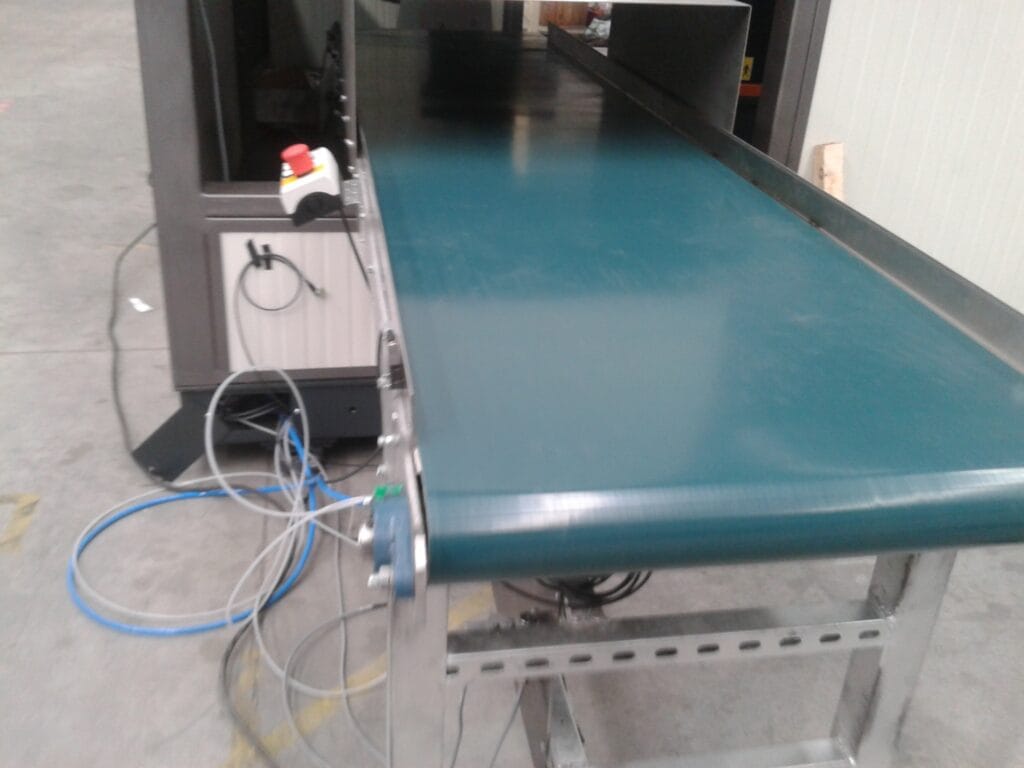
Belt conveyors
For horizontal and inclined conveying of materials.
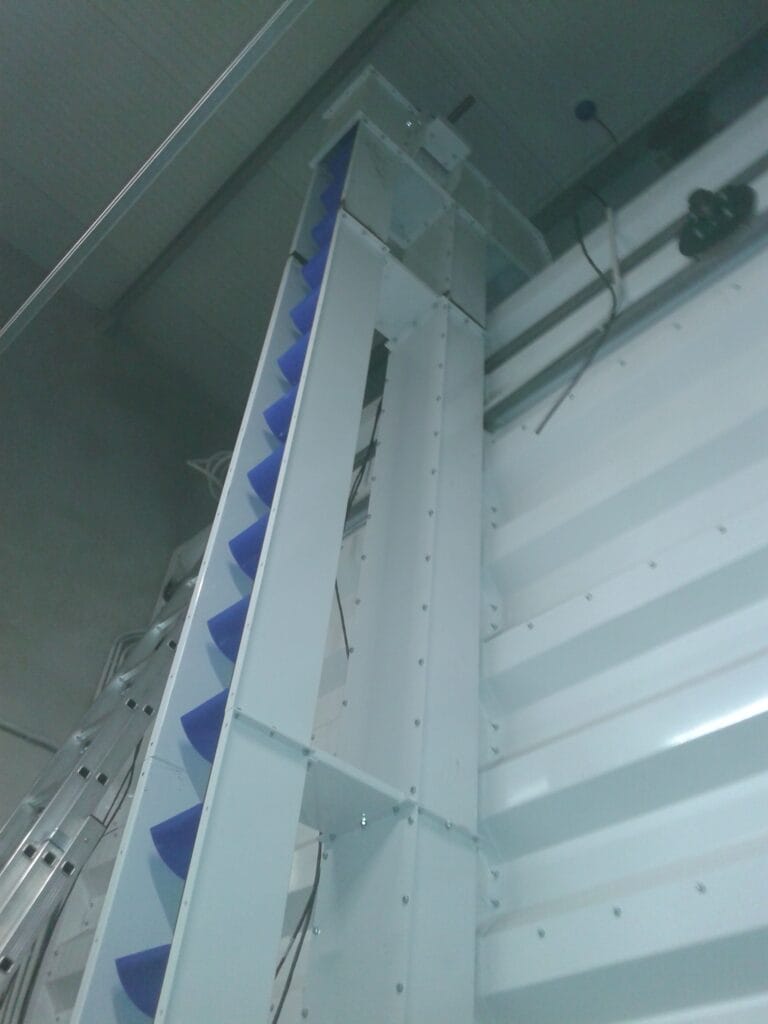
Bucket elevators
Vertical conveying of grain, cement and other materials.
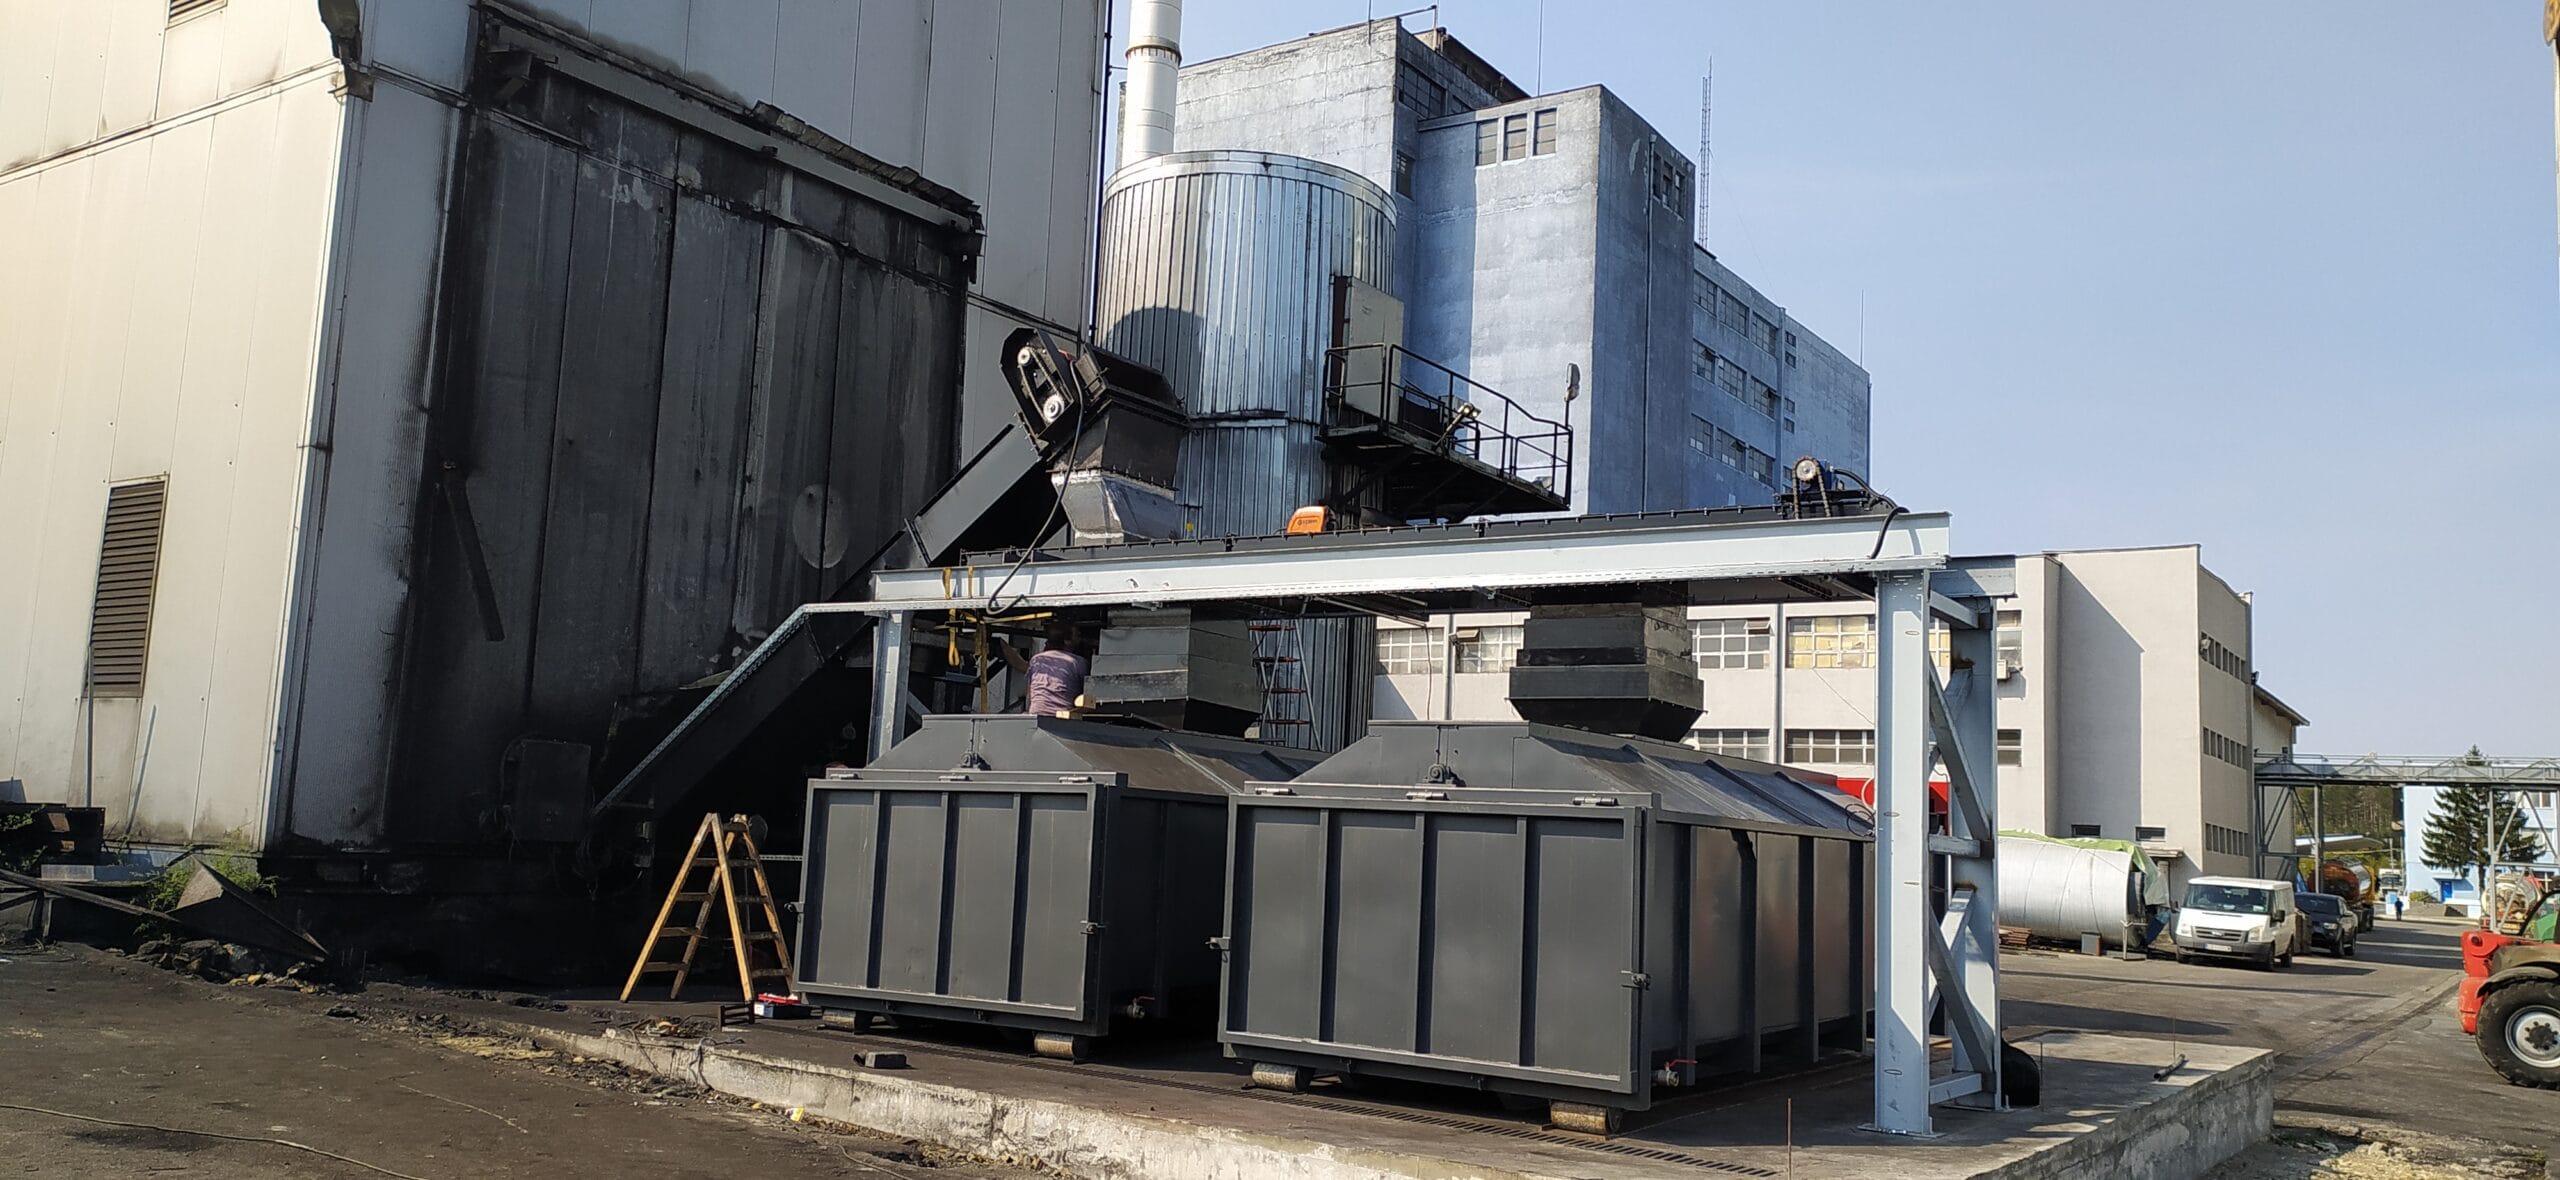
Chain conveyors
For heavy materials and continuous operation.
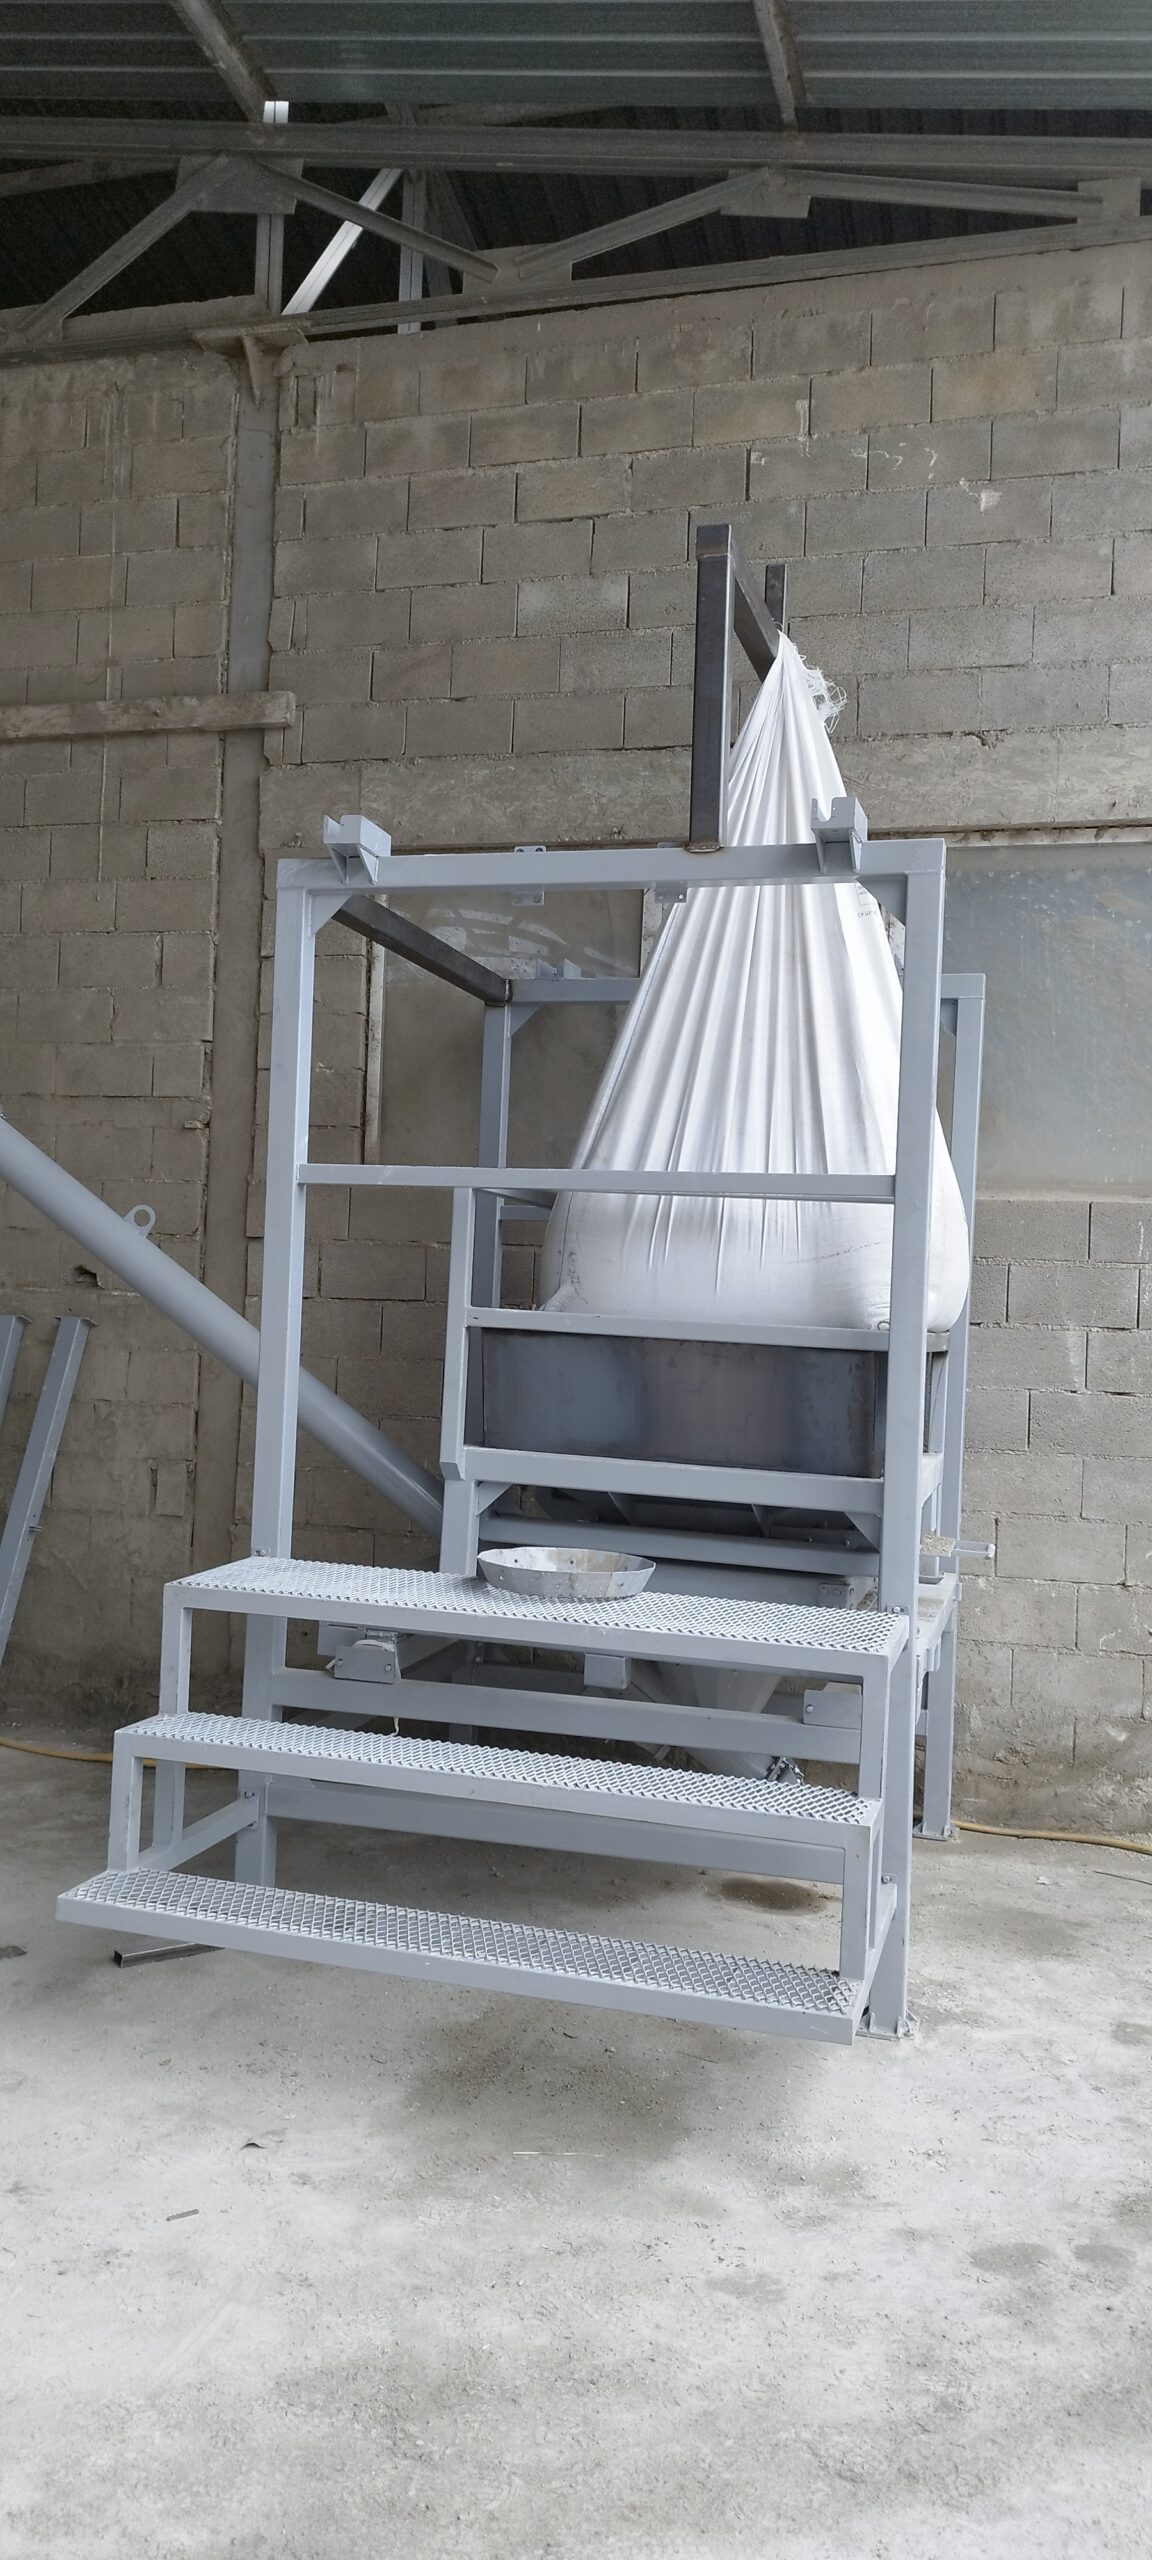
Big bag stations
For filling and discharging big bags (FIBCs).
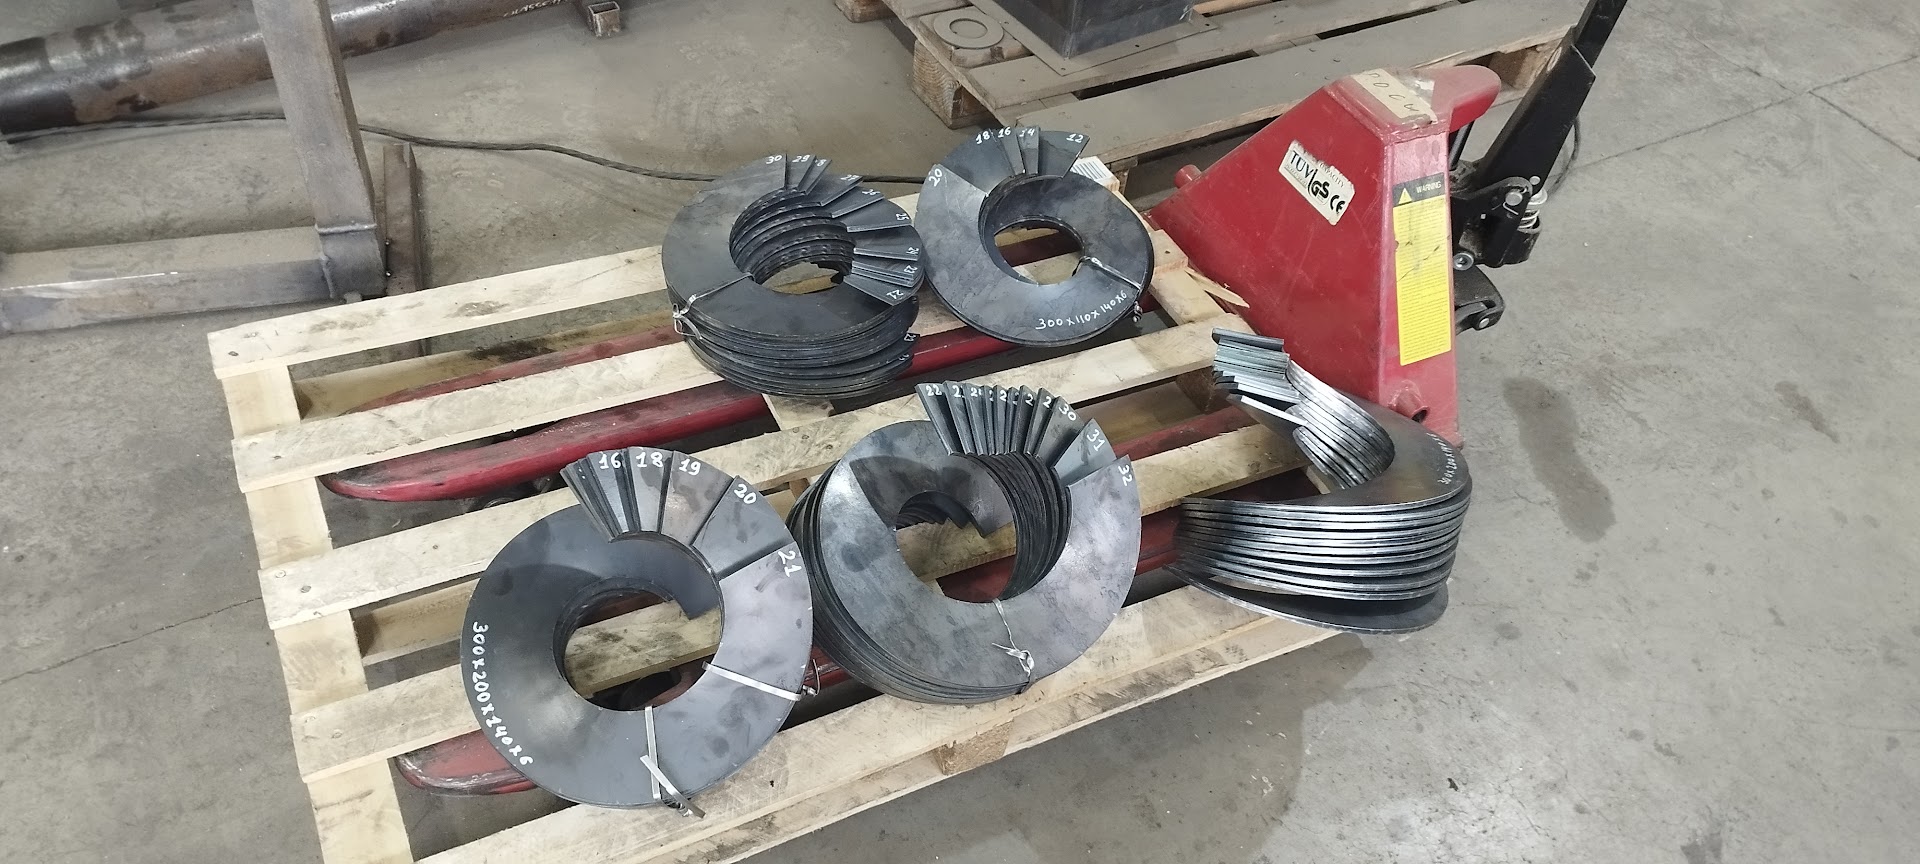
Screw flights and segments
We manufacture screw flights and flight segments.
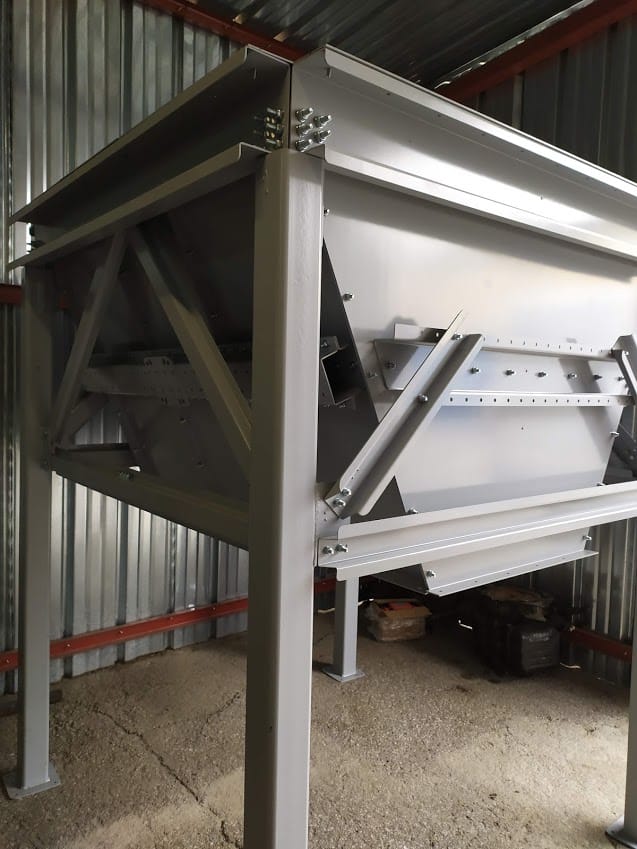
Hoppers
Steel hoppers for storing and feeding bulk materials.
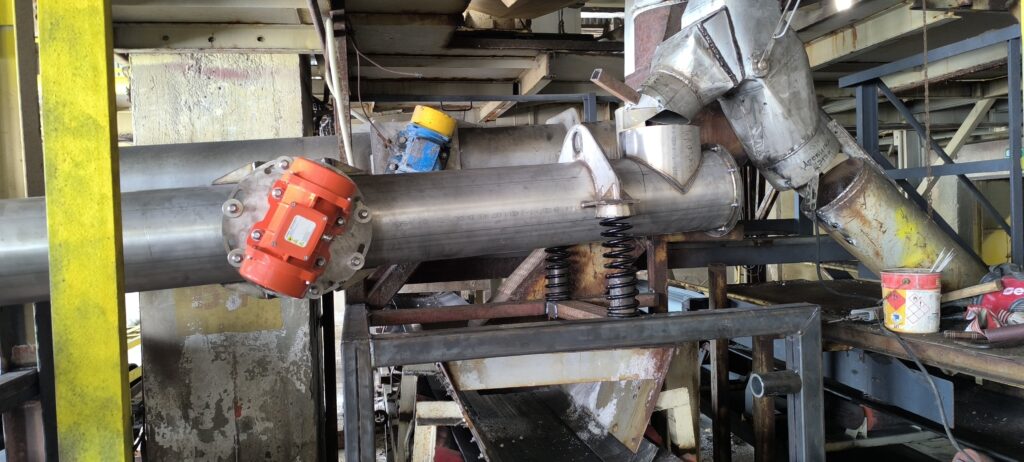
Vibratory conveyors
For metered feeding of free-flowing and abrasive materials.
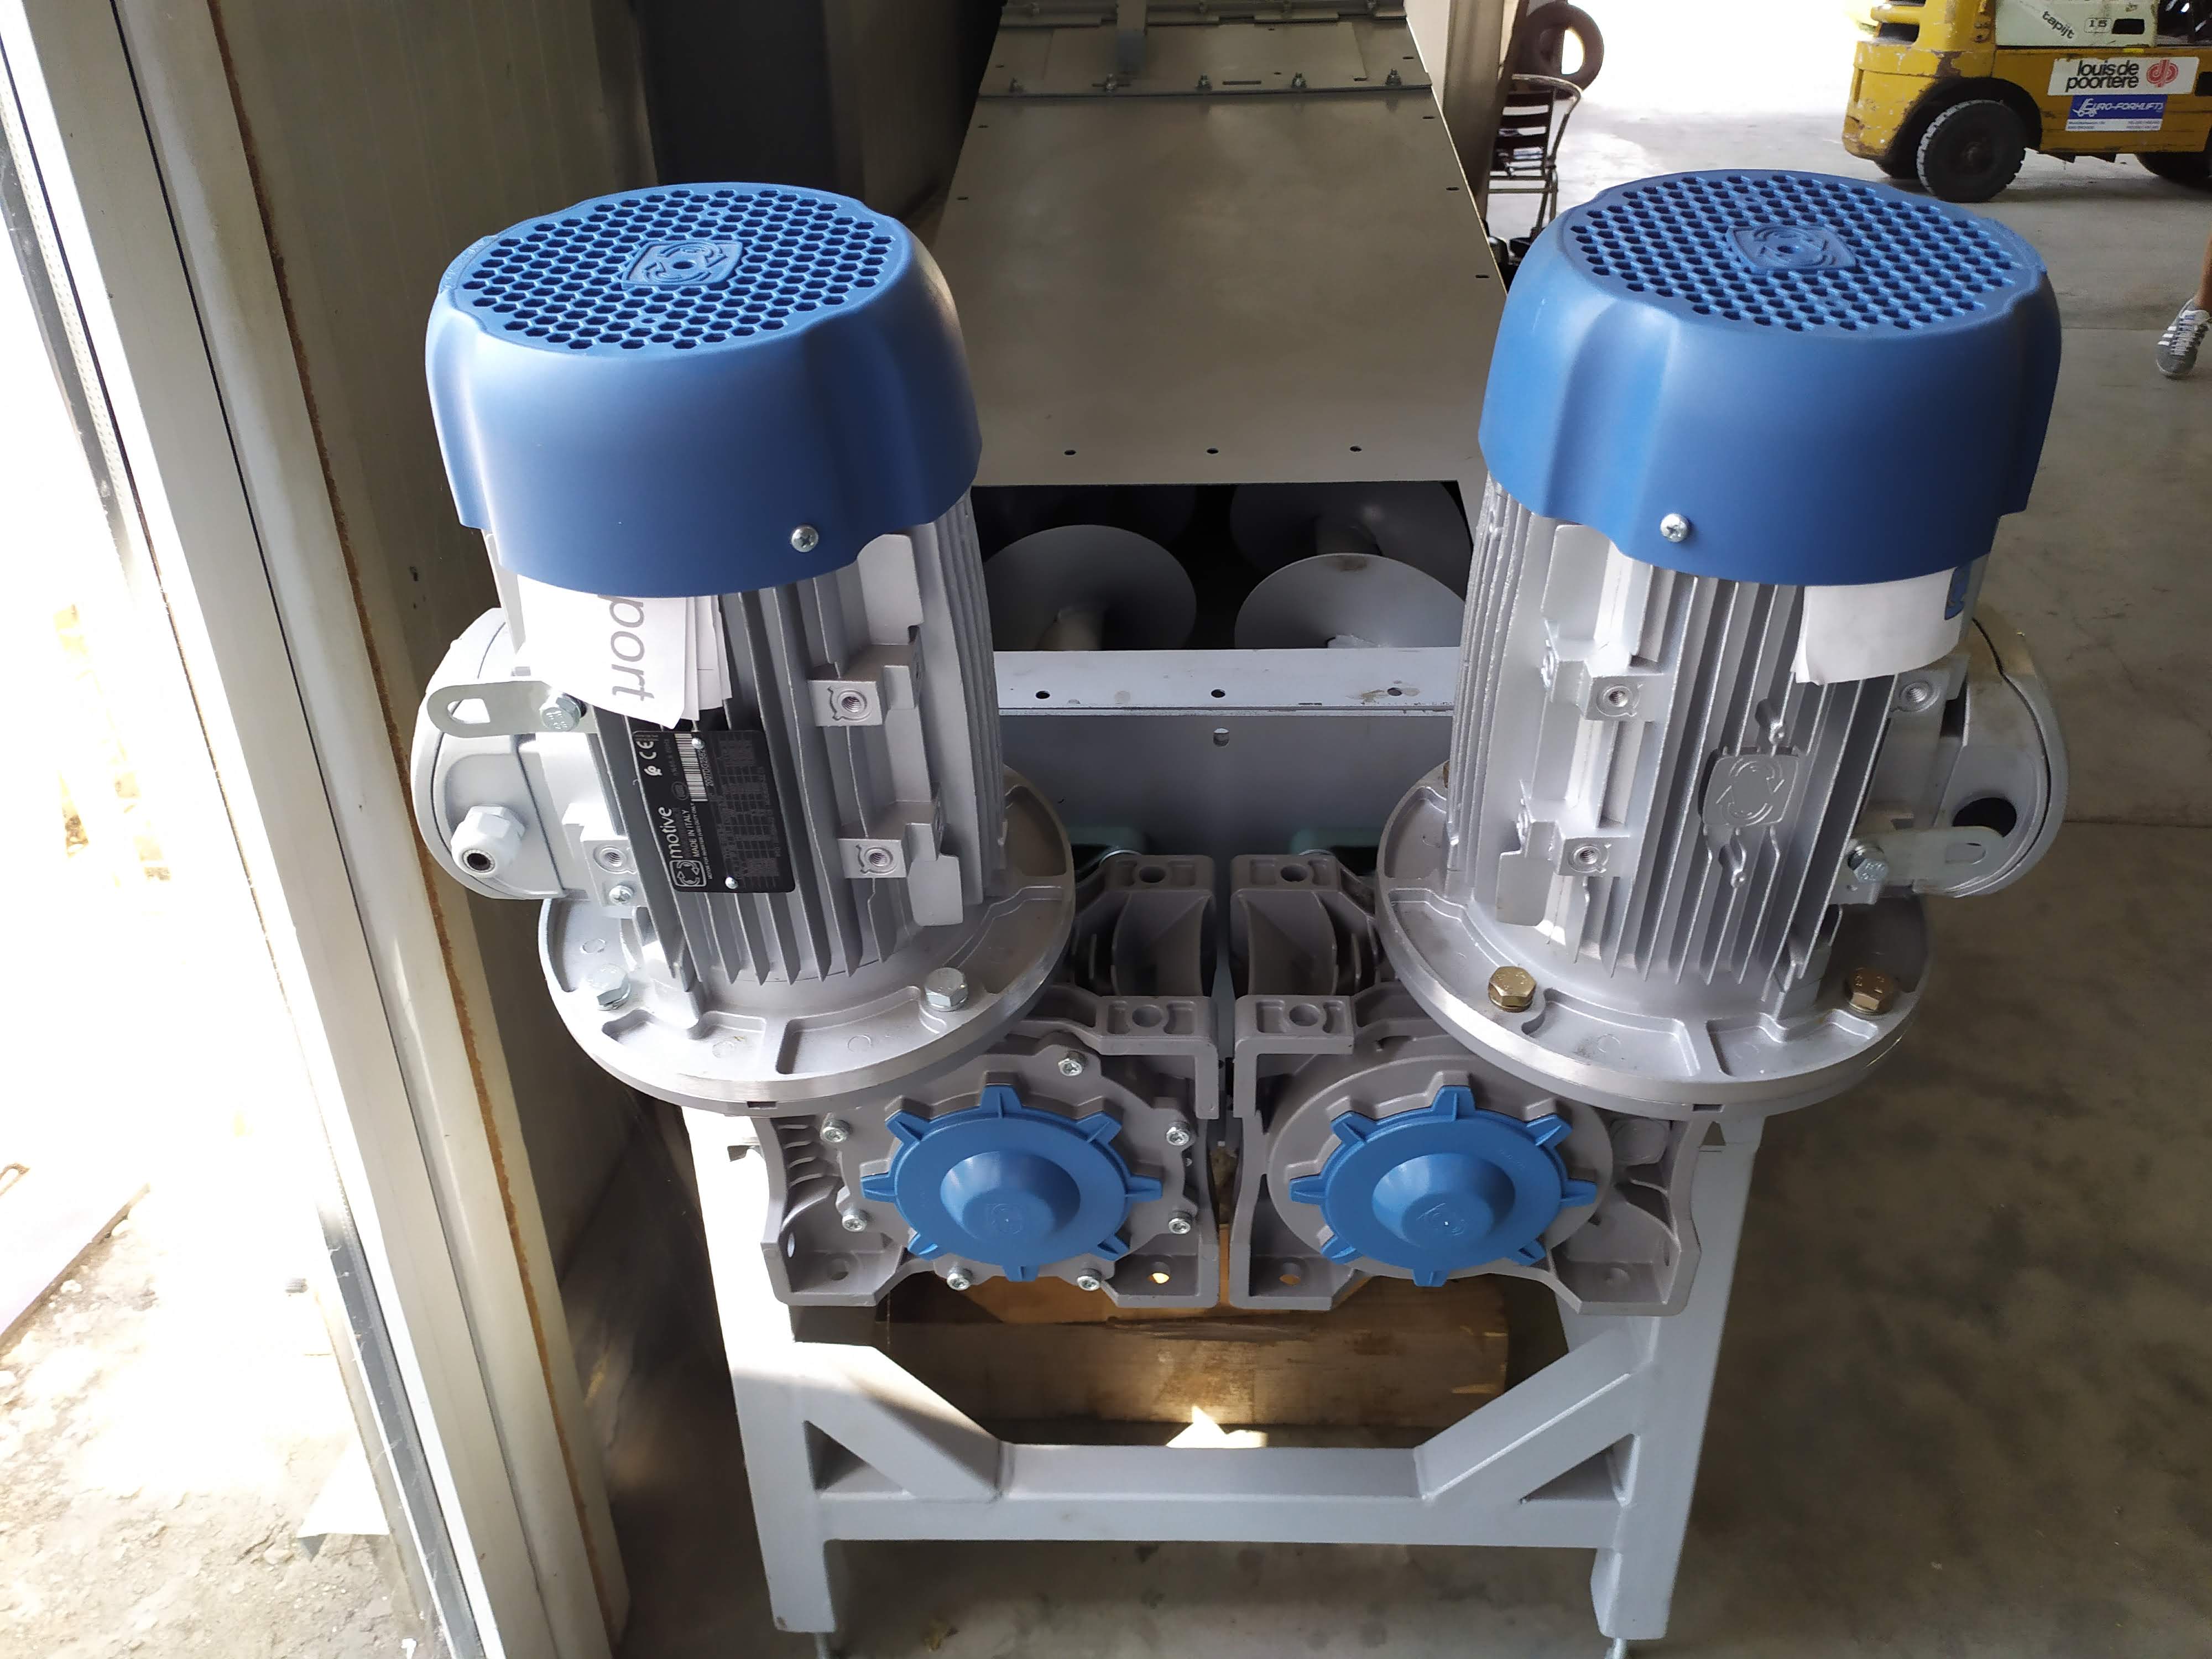
Screw mixers
For continuous mixing of bulk and powdered materials.
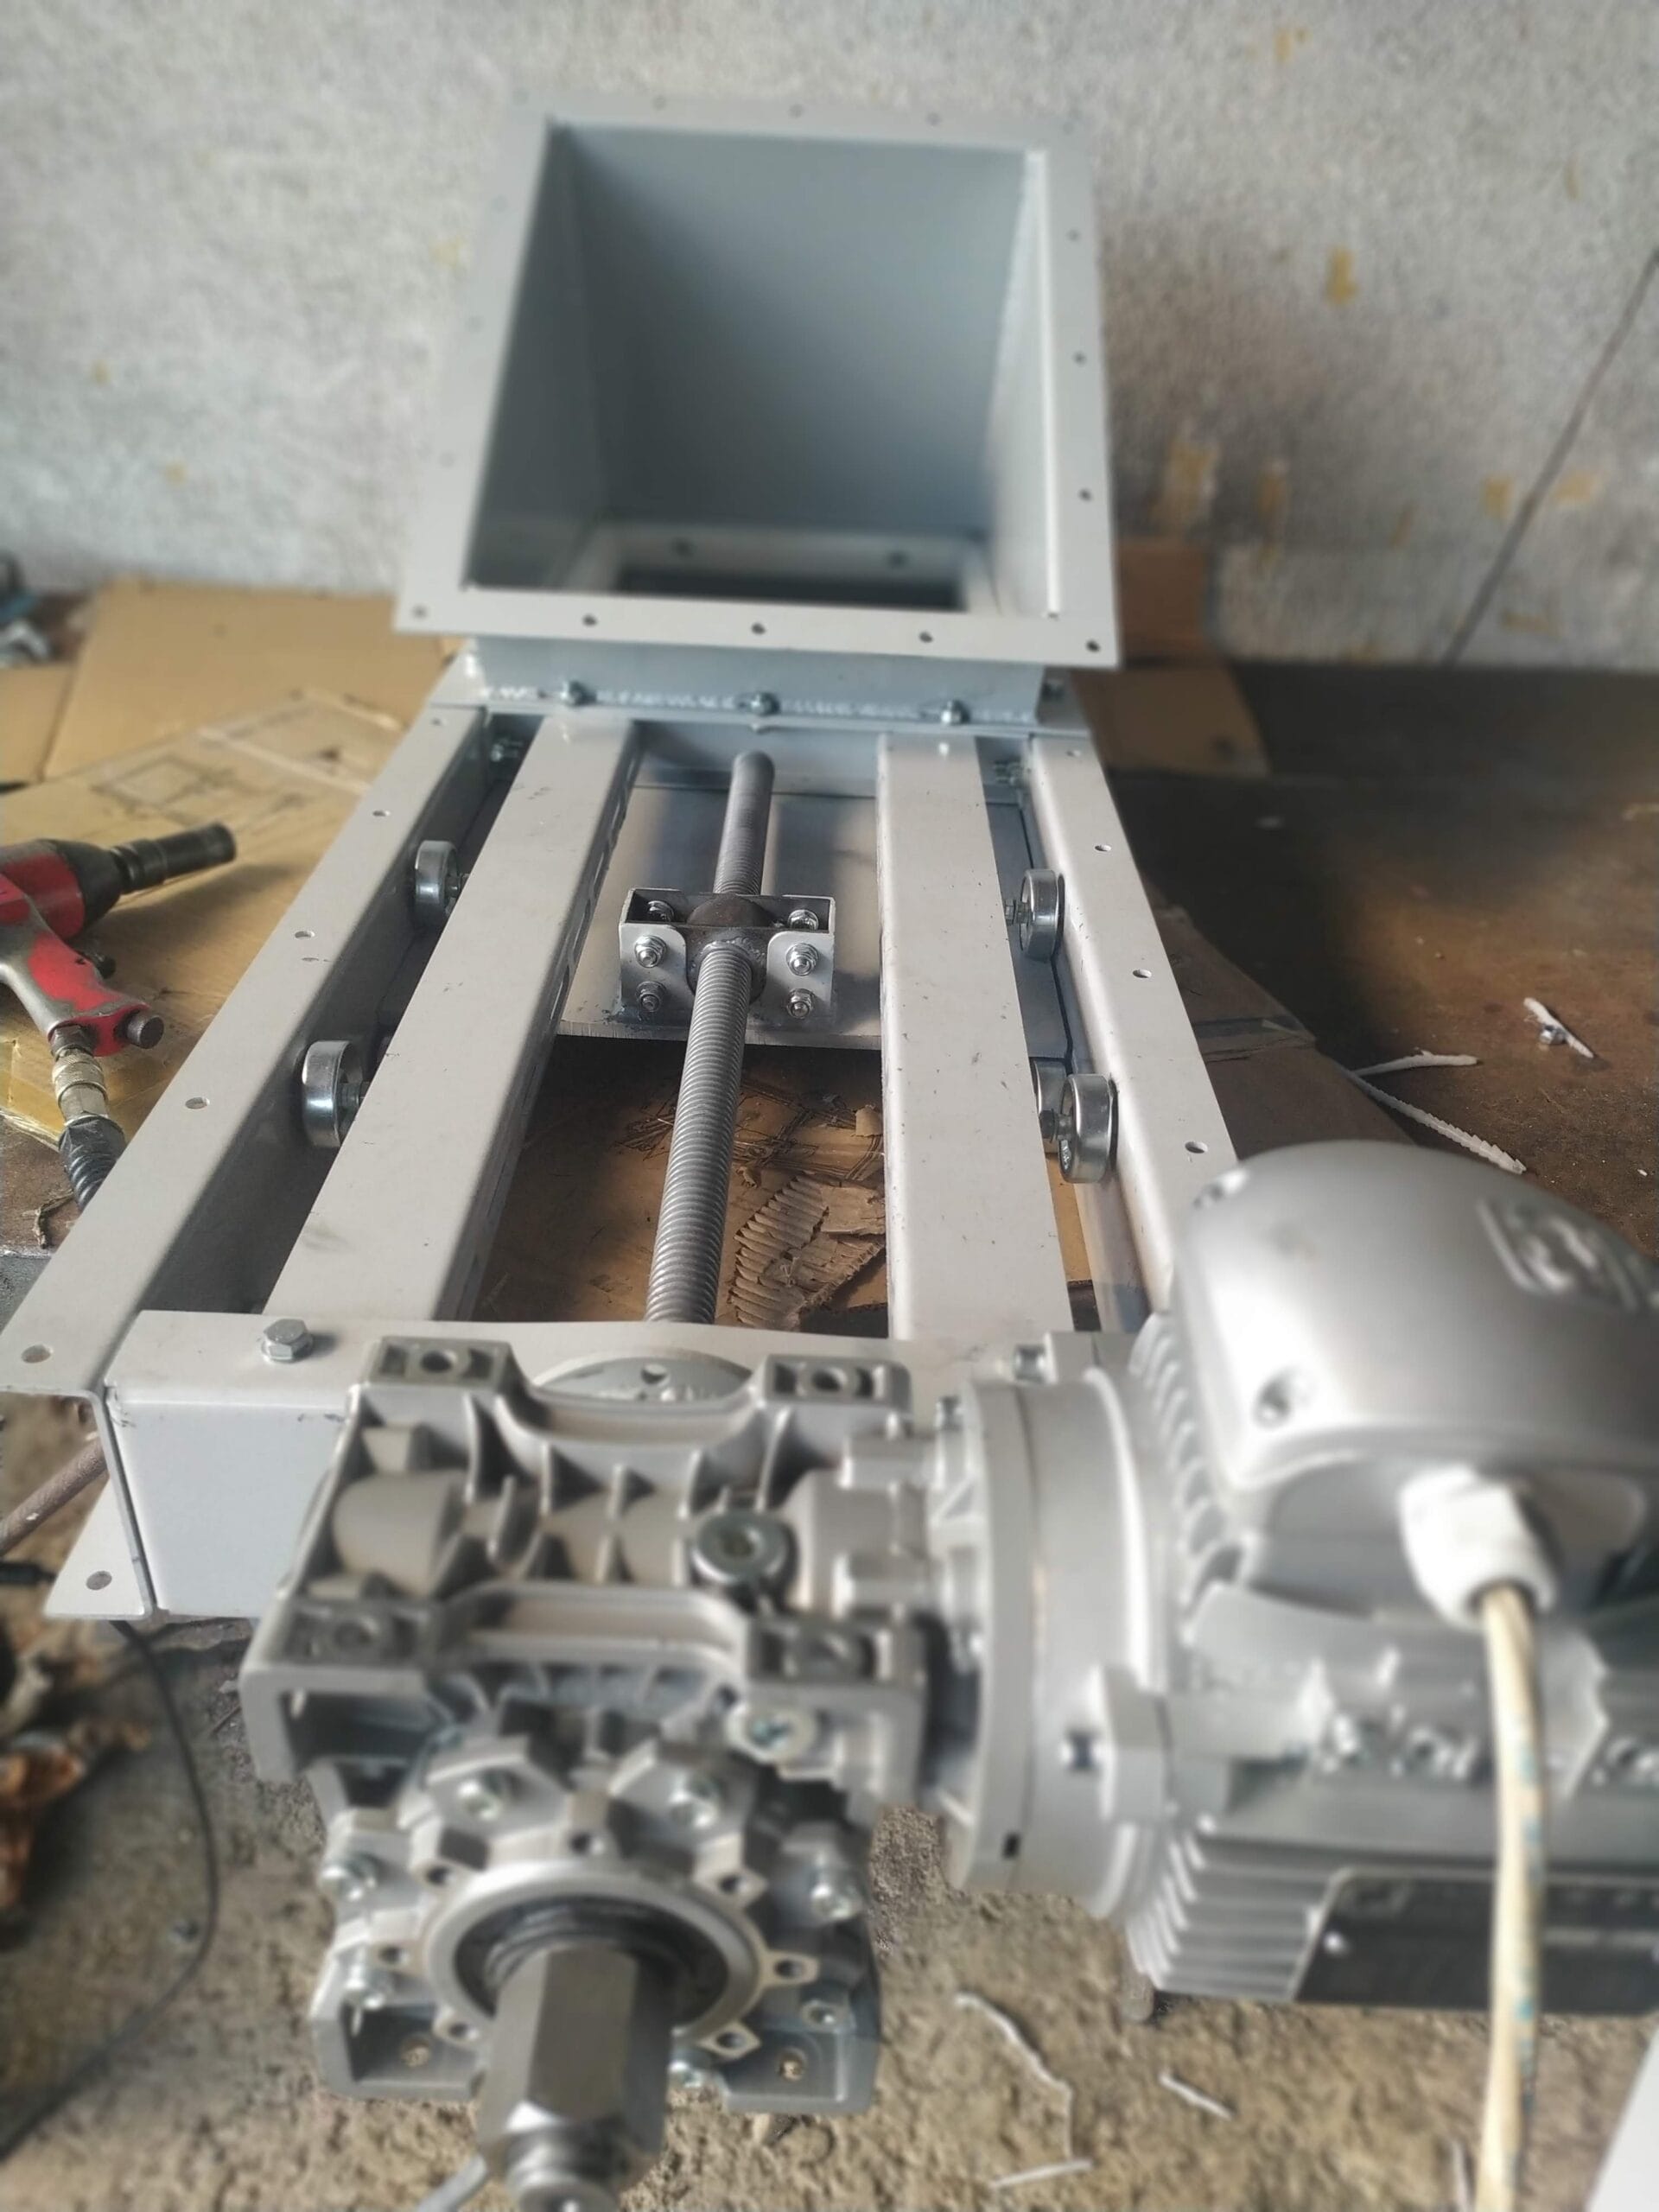
Slide gate valves
For shutting off and regulating material flow below hoppers, silos and conveyors.
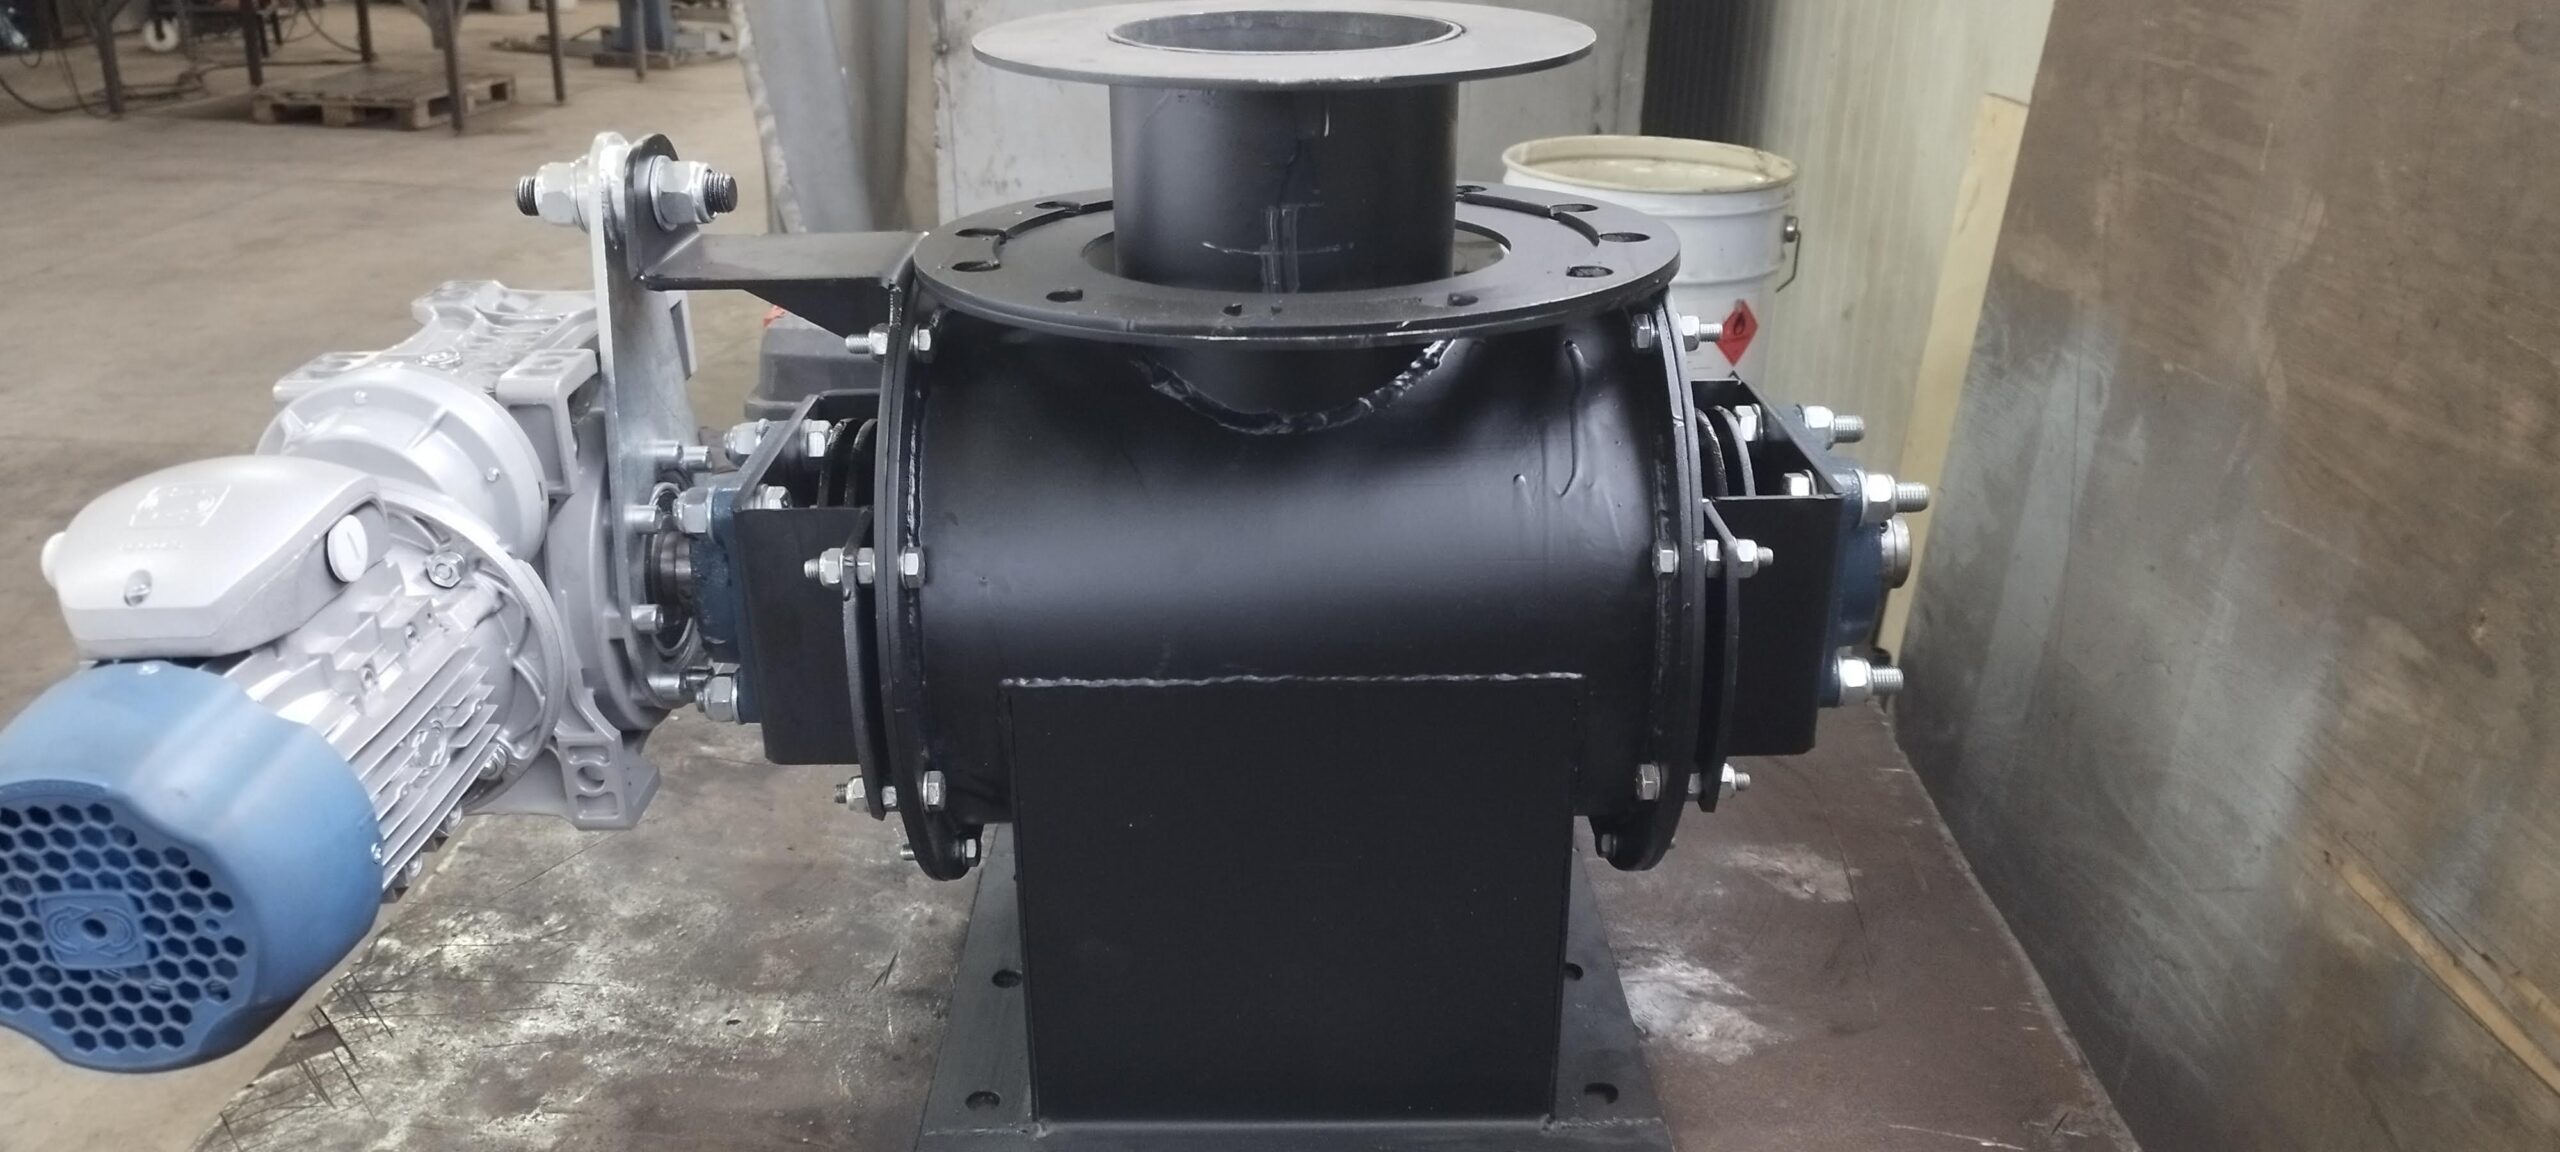
Rotary valves
For controlled feeding and dosing of bulk and powdered materials.
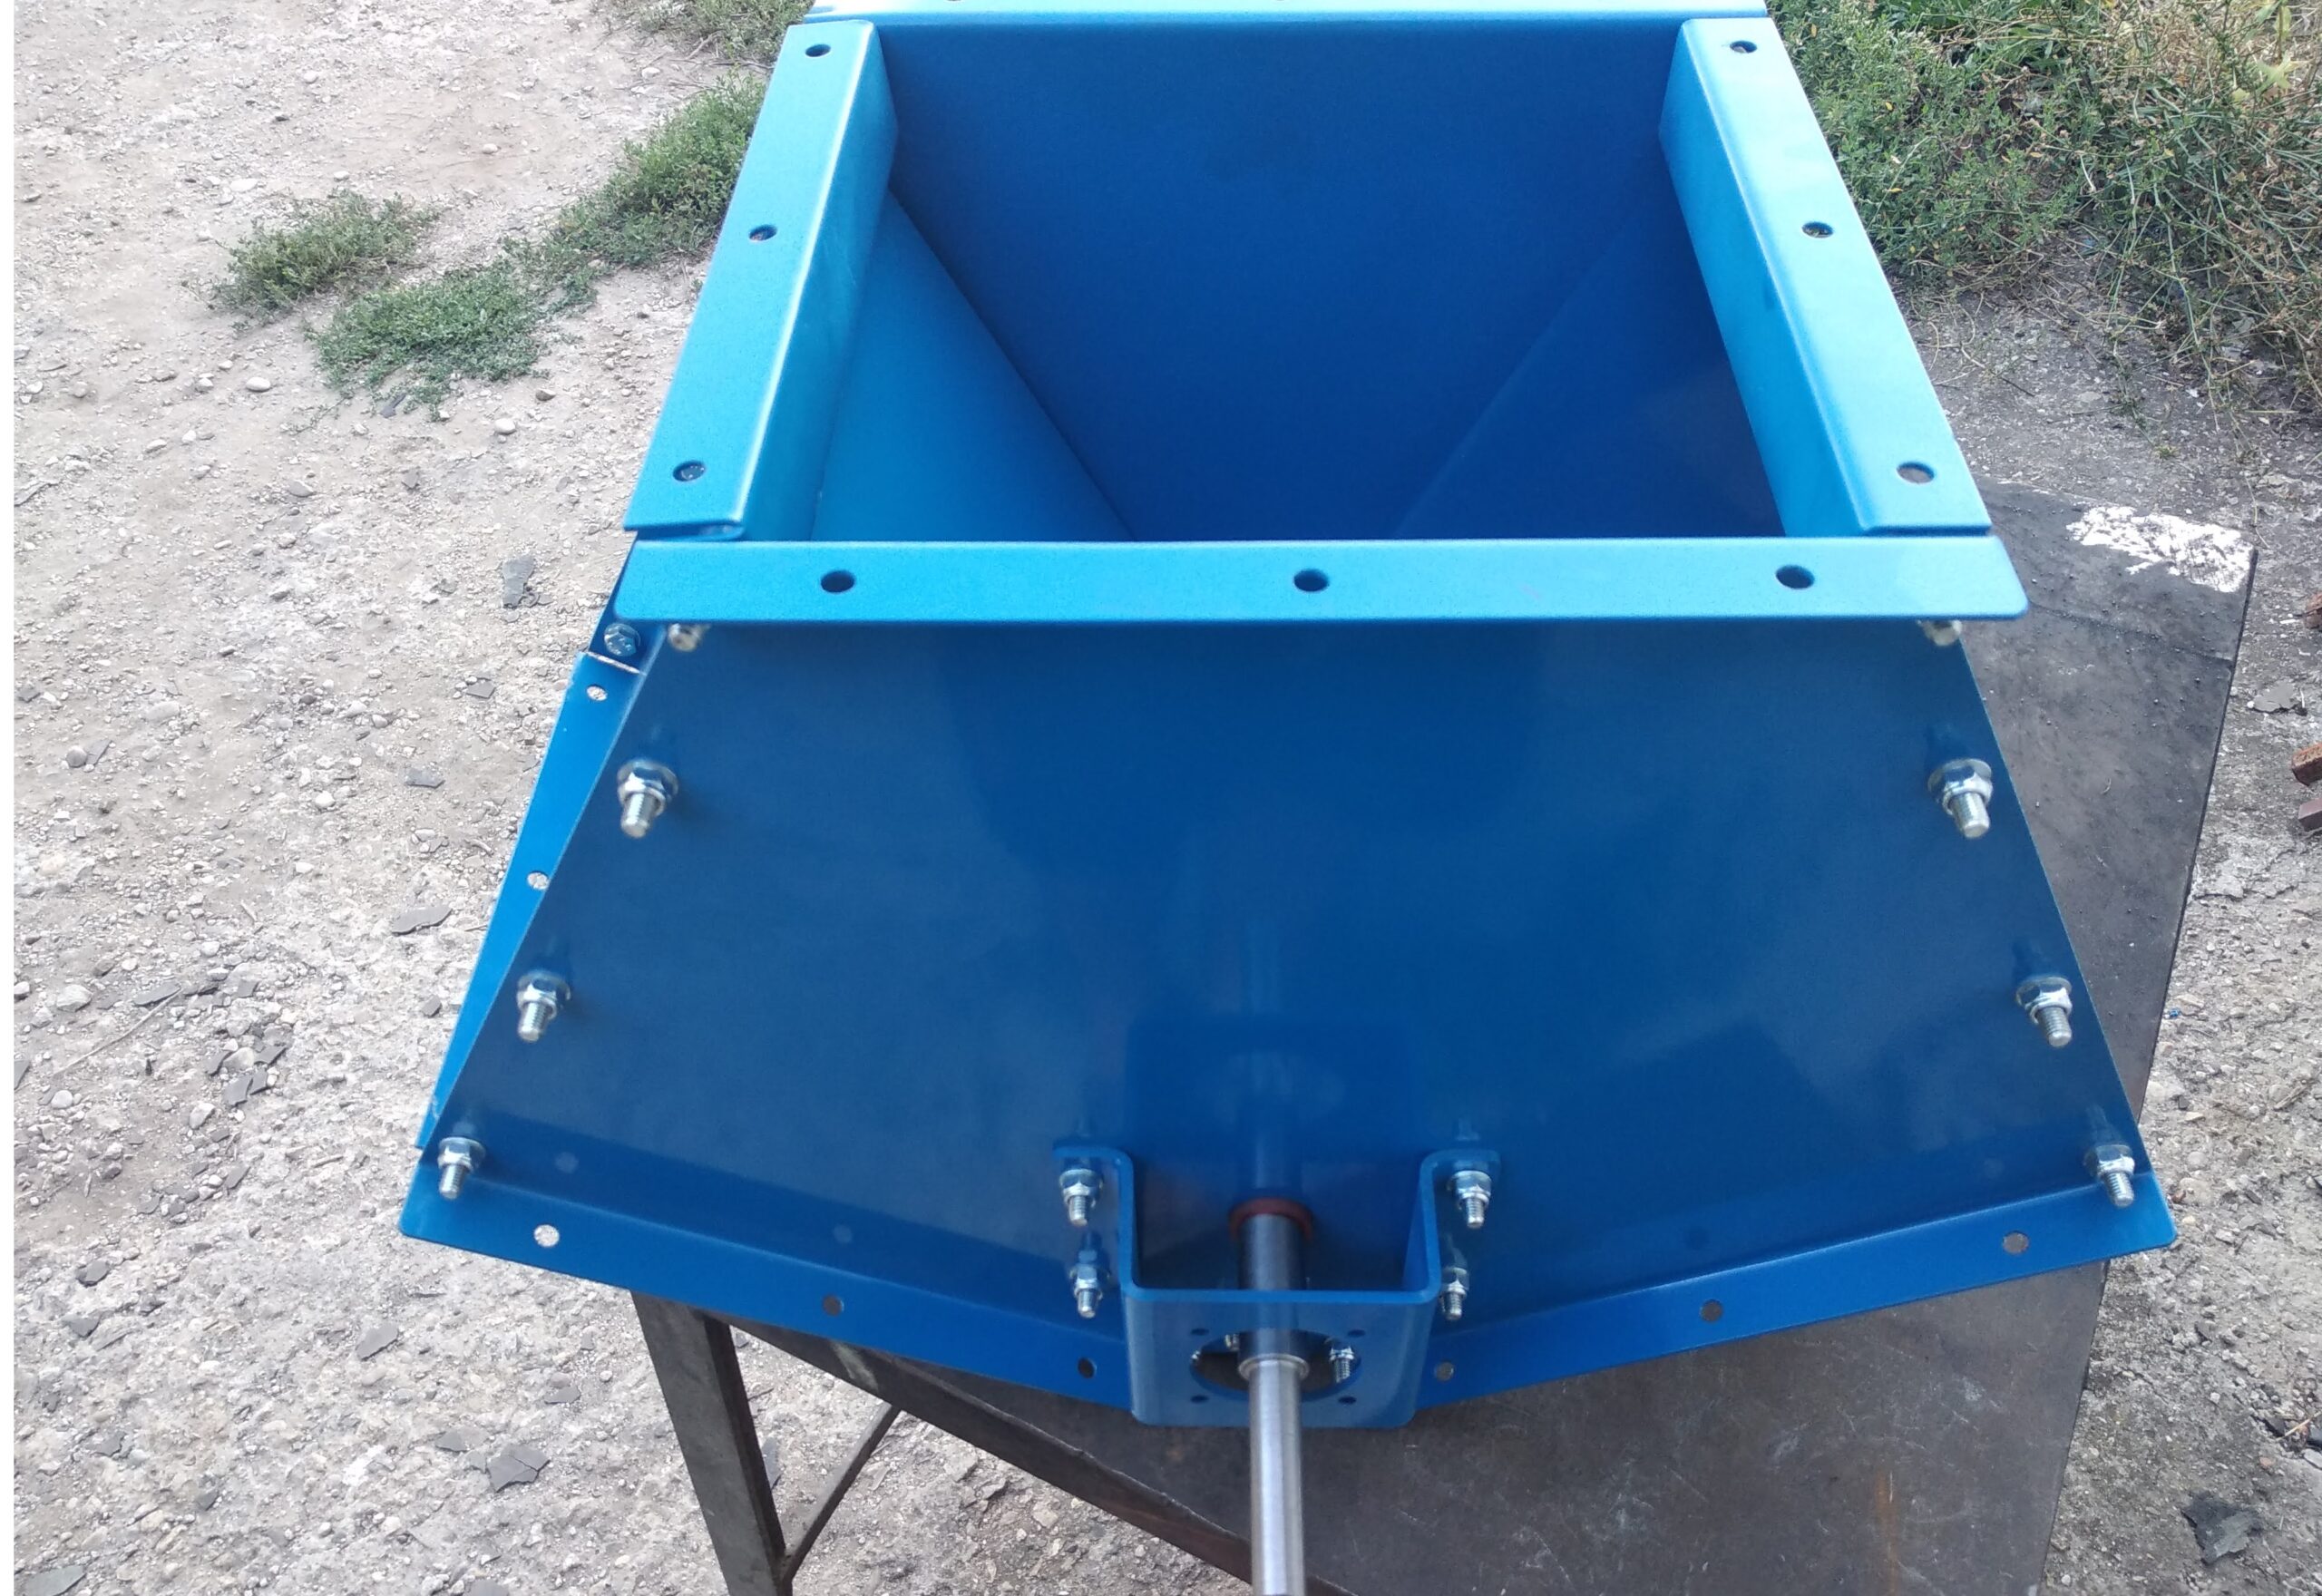
Diverter valves
For directing and regulating the flow of bulk and powdered materials.
Can’t find exactly what you need?
We build to order. Send us the material, the capacity and the length or height, and we will propose a solution with an offer.
Our equipment handles powdered, granular and bulk materials such as cement, sand, grain, feed, ash and other raw materials. It is used in the cement, agricultural, food and processing industries, where accuracy and a stable process are essential.
The range includes screw conveyors, bucket elevators, chain and belt conveyors, slide gate valves, hoppers, rotary valves, diverter valves and auxiliary equipment. They can be combined into complete systems or used as stand-alone machines. Each type comes in different configurations depending on capacity, length, working environment and control method.
The design takes into account the abrasiveness of the material, moisture, temperature and any hygiene or sealing requirements. This lets us adapt the equipment both to standard industrial conditions and to more demanding applications.